

¿Cuándo es mejor un centro de mecanizado de perfiles que un VMC estándar para piezas largas de aluminio?
¿Cuándo es mejor un centro de mecanizado de perfiles que un VMC estándar para piezas largas de aluminio?
Las piezas de aluminio largas pueden exceder el área de trabajo práctica de un centro de mecanizado vertical (VMC).1. Las preparaciones adicionales aumentan el trabajo de manipulación y alineación,2, por lo que la selección de la máquina debe comenzar con el proceso completo.
Un centro de mecanizado de perfiles es mejor cuando su longitud de mecanizado útil, los soportes de perfil y el acceso a múltiples caras eliminan las preparaciones repetidas que requeriría un VMC estándar. La ventaja depende de la pieza real, los dispositivos de sujeción, las tolerancias y la carga de corte. Ambas máquinas deben compararse según los mismos requisitos de producción.
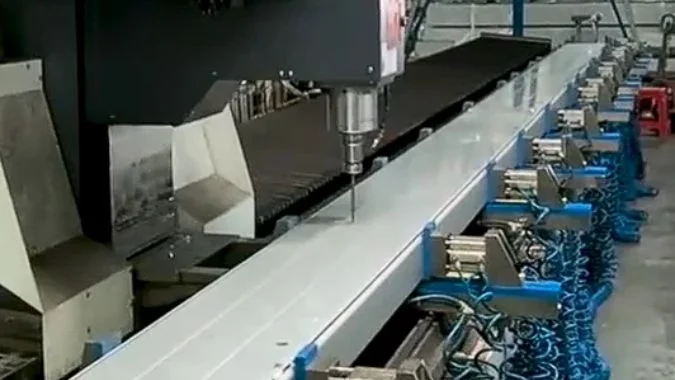
Una extrusión larga puede contener una fila de agujeros, una ranura continua y características en caras opuestas. Cada característica tiene una ubicación vinculada a la referencia de la pieza. La comparación de máquinas comienza con un dibujo superpuesto al dispositivo de sujeción propuesto. Ese diseño muestra qué características permanecen accesibles y qué operaciones obligarían a un cambio de preparación.
¿Qué requisitos de mecanizado de piezas largas pueden hacer que un centro de mecanizado vertical (VMC) estándar sea poco práctico?
Una pieza puede caber en la mesa de un VMC y aun así ser difícil de mecanizar. Las trayectorias de herramienta y las posiciones de soporte requeridas revelan los límites prácticos.
Un VMC estándar se vuelve poco práctico cuando las características críticas exceden su área de corte accesible, las preparaciones repetidas no pueden cumplir con los requisitos de alineación o el perfil largo no puede ser soportado de forma segura. Un centro de mecanizado de perfiles ofrece una ventaja cuando su bancada, abrazaderas y configuración de ejes cubren esos requisitos en una sola preparación.
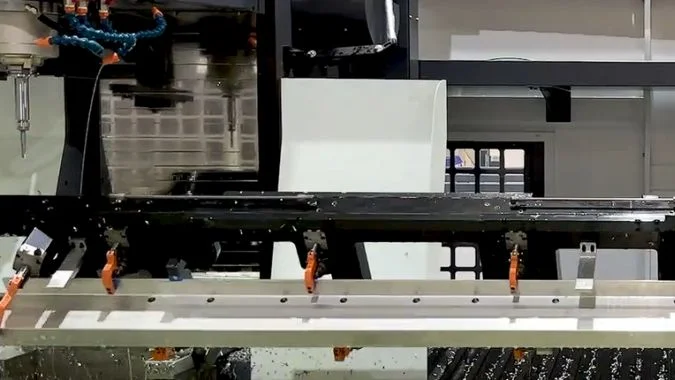
El rango de características determina el alcance requerido.
La longitud de la pieza y la longitud de mecanizado requerida pueden diferir. Una extrusión larga con todo el mecanizado cerca de un extremo puede seguir siendo práctica en un VMC con el soporte y el espacio libre adecuados. Una ranura continua o un patrón de agujeros que abarque la mayor parte de la extrusión crea un requisito diferente,3. La fresa debe alcanzar todo el rango de características en una configuración controlada.
La comparación debe incluir la mesa, la carcasa, la ruta de carga y el espacio para el voladizo soportado. El perfil debe permanecer libre de la estructura de la máquina durante todo el movimiento.
| Requisito de producción | Límite práctico a comprobar en el VMC | Ventaja potencial del centro de mecanizado de perfiles |
|---|---|---|
| Un patrón de agujeros abarca la pieza | La herramienta no puede alcanzar ambos extremos en una sola preparación | Un rango de mecanizado útil más largo cubre el patrón |
| Una ranura continua cruza los límites de la preparación | Los cortes separados requieren una alineación cuidadosa | Una trayectoria de herramienta evita una unión entre configuraciones |
| Las características superiores y laterales comparten una referencia | Girar la pieza requiere otra alineación | El cabezal o sistema de indexación seleccionado proporciona acceso |
| Un perfil hueco se flexiona bajo la carga de corte | Las posiciones de soporte son limitadas | Los soportes distribuidos sujetan el perfil cerca del corte |
El acceso frontal y la manipulación afectan la producción por lotes
Las características superiores y laterales requieren un método de acceso confirmado. Un husillo giratorio, un cabezal angular o un dispositivo de indexación pueden reducir el giro y la re-sujeción. La configuración seleccionada debe alcanzar las caras especificadas con las herramientas reales.
Un perfil estacionario y una unidad de mecanizado móvil pueden simplificar el soporte a lo largo de una bancada larga4. Los soportes aún deben resistir las fuerzas de corte sin aplastar las paredes huecas.
Las comparaciones de lotes deben contar la carga, la alineación, el movimiento de la sujeción, el mecanizado y la descarga. Un centro de mecanizado vertical (VMC) sigue siendo adecuado cuando las características encajan, el dispositivo es estable y el ciclo completo satisface las necesidades de producción.
¿Cómo puede el reposicionamiento repetido afectar al espaciado de los orificios y a la alineación de las características?
Cada nueva configuración puede cambiar la ubicación de la pieza y la forma soportada. Los errores de montaje se vuelven más difíciles de diagnosticar, por lo que la comparación debe rastrear las características a través de los límites de configuración.
El reposicionamiento repetido puede desplazar o rotar la referencia de la pieza y cambiar su forma soportada. El espaciado de los orificios entre diferentes configuraciones y la alineación entre ranuras o caras pueden variar. Las características producidas dentro de una configuración pueden permanecer precisas entre sí, incluso cuando todo el grupo está mal ubicado.
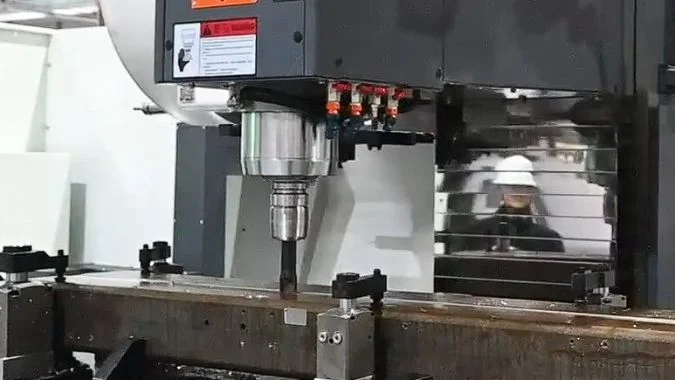
Una referencia desplazada afecta las relaciones entre configuraciones
Un grupo de orificios puede tener el espaciado interno correcto y aun así quedar en la posición incorrecta con respecto al extremo lejano del perfil. Esto sucede cuando la segunda configuración establece una referencia diferente.
La alineación angular también es importante. Una pequeña rotación durante la re-sujeción crea una mayor diferencia lateral más lejos del punto de referencia5. Una ranura larga puede mostrar un escalón en la unión entre dos posiciones de mecanizado.
| Cambio durante el reposicionamiento | Posible efecto en la pieza | Inspección útil |
|---|---|---|
| La posición del tope longitudinal cambia | Los grupos de orificios se acercan o se alejan entre sí | Distancia entre orificios de diferentes configuraciones |
| El perfil rota ligeramente | Las ranuras o filas de orificios pierden la alineación | Alineación en todo el rango especificado |
| La presión de sujeción cambia | Las paredes delgadas se mueven durante el corte | Dimensions in the required inspection condition |
| Support locations change | The profile bends differently | Feature position and shape after release |
Machine repeatability and setup repeatability need separate checks
Axis repeatability describes repeated machine positioning under defined test conditions6. It does not include every change caused by moving the workpiece, cleaning a stop, or tightening a clamp.
Repositioning errors can combine, but they do not always grow by the same amount or in the same direction. Inspection should cover critical relationships across setups, including distances between widely separated holes7.
A single setup removes repeated datum establishment. It still requires accurate axis motion, suitable support, and controlled clamping. The finished profile should be measured in the condition required by the drawing. This check reveals distortion that becomes visible after the clamps release.
¿Por qué debería evaluarse el recorrido del eje X junto con el ancho del perfil y la altura de la fijación?
A long X-axis can still leave side features unreachable. Width, height, and tool clearance need a combined layout before the machine size is accepted.
X-axis travel must be checked with profile width, fixture height, and the complete tool assembly because all three determine the reachable cutting area. The layout must cover every feature, approach move, and retract. Width affects side access, and fixture height changes tool reach and clearance.
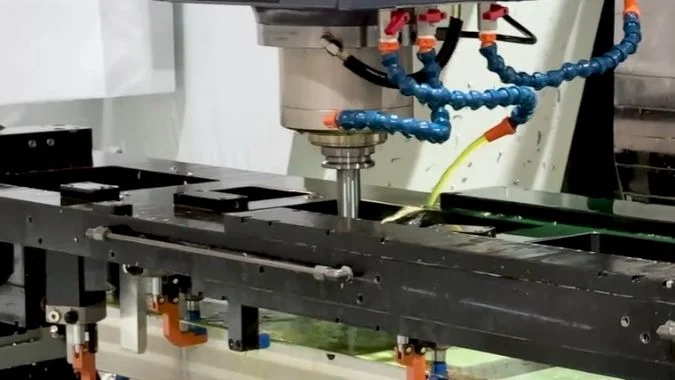
The complete setup defines the working area
Nominal axis travel describes machine movement. The usable machining area also depends on the part position, clamps, tool length, and head orientation.
The required X movement comes from the extreme tool-center positions along the planned paths. Cutter offsets, approach moves, and end-face access can extend those positions beyond the feature edges. Fixture components also restrict where the part can sit.
| Layout item | Dimensions or movements to check | Problem the check can reveal |
|---|---|---|
| X-axis coverage | First and last tool-center positions, approach, and overtravel | An end feature remains outside the reachable range |
| Profile and fixture width | Y movement, clamp width, and tool assembly clearance | Side cutting or edge milling causes interference |
| Fixture and profile height | Spindle-nose distances, tool length, and retract clearance | The tool cannot reach or retract safely |
| Tilted or angular tooling | Head housing, holder, and cutter envelope | The cutter reaches the face but the housing collides |
| Clamp movement | Clamp positions throughout the machining sequence | A clamp blocks a feature or leaves poor support |
Height affects both reach and clearance
A taller fixture may improve access to a side face, but it also reduces clearance above the part. A longer tool may reach a deep feature, but the holder can still strike the profile or a clamp.
Profile width mainly affects Y coverage in a conventional lengthwise setup. It does not automatically consume a fixed amount of X travel. The actual orientation determines the space needed.
A supplier should check the complete part, fixture, and tool assembly against the machine layout. A clearance check should include both ends and every required face. A trial cut can then confirm the features with the tightest access.
¿Qué operaciones de fresado y roscado requieren algo más que una alta velocidad máxima de husillo?
A fast spindle can still stall, vibrate, or damage taps under the wrong load. The demanding operations should determine the required torque, support, and control capability.
Wide slots, deep pockets, large holes, and larger threads require usable spindle torque, stable tooling, and effective chip removal. Thin walls require close support and controlled cutting forces. Rigid tapping also requires spindle and feed-axis synchronization through entry, reversal, and withdrawal. Maximum RPM does not establish these capabilities.
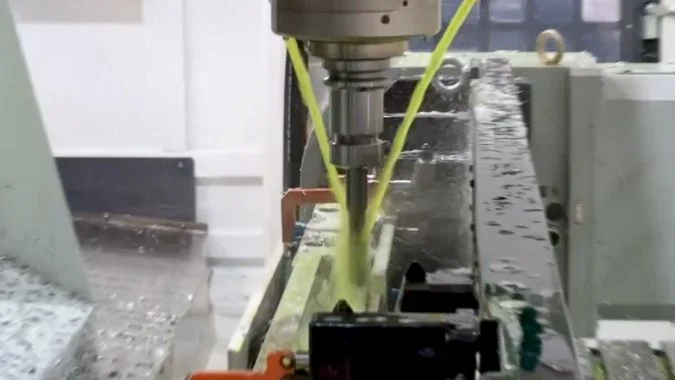
Cutting performance depends on the operating speed and setup
Spindle torque should be checked at the planned milling or tapping speed. The maximum power rating may describe a different operating point8. A trial should use the intended cutter engagement, tool overhang, profile supports, and chip-clearing arrangement.
Thin walls add another limit. A rigid machine can still deflect an unsupported profile wall9. Clamp position, support shape, tool sharpness, and cutting force all affect the result.
| Operación | Capability beyond maximum RPM | Evidence from a trial |
|---|---|---|
| Wide slots or deep pockets | Available power and torque, stable engagement, chip removal | Stable load and acceptable slot size and finish |
| Thin-wall milling | Local support, controlled force, and suitable tooling | Wall thickness and shape remain within tolerance |
| Large-hole drilling or larger-thread tapping | Torque at the selected speed and effective lubrication | Stable cutting and conforming holes or threads |
| Rigid tapping | Coordinated spindle and feed-axis movement | Consistent thread quality through repeated cycles |
| Many scattered holes and tool changes | Axis response and complete sequence efficiency | Measured part cycle time |
Rigid tapping requires the correct relationship between rotation and feed
Rigid tapping advances the tool by one thread lead per spindle revolution10. For a standard single-start thread, the lead equals the pitch11.
In metric feed-per-minute programming, the relationship is F = n × P. F is the feed in mm/min, n is spindle speed in rpm, and P is pitch in mm. In feed-per-revolution programming, the commanded feed equals the pitch for that thread.
The controller must maintain synchronization during acceleration, reversal, and withdrawal. The supplier should confirm tapping capability for the actual thread size, material, depth, and holder.
A useful comparison includes the hardest recurring slot and thread on the production profile. Inspection should cover the least supported section. Timing should include tool changes and any clamp repositioning needed to complete the part.
Conclusión
A profile machining center earns its advantage through full feature access, stable support, fewer setups, and proven cutting performance across the actual long aluminum part.
-
"Vertical Machining Center (VMC) Technical Specifications:", https://www.rknec.edu/wp-content/uploads/2024/02/Spcifications_Vertical-Machining-Center.pdf. Standard VMCs typically offer X-axis travel ranging from 500mm to 1500mm, with larger models extending to 2000mm, though actual usable machining length is reduced by fixturing requirements and tool approach distances. Evidence role: general_support; source type: education. Supports: typical working area dimensions and travel ranges for standard vertical machining centers. Scope note: Specific capacity varies by manufacturer and model class ↩
-
"A Novel High-Precision Workpiece Self-Positioning Method for … – PMC", https://pmc.ncbi.nlm.nih.gov/articles/PMC12299440/. Manufacturing studies indicate that setup and changeover activities can account for 20-30% of total production time in multi-setup machining operations, with alignment verification adding measurable cycle time. Evidence role: general_support; source type: research. Supports: the productivity impact of multiple setups in CNC machining operations. Scope note: Actual impact varies with part complexity, tolerance requirements, and operator skill ↩
-
"CNC Trick to Machine a Massive 60” Part", https://www.youtube.com/watch?v=rA2vRwCFC3M. Technical literature on long-part machining identifies continuous features as particularly challenging because they require uninterrupted tool paths, consistent support along the cutting zone, and elimination of setup transitions that could create visible steps or alignment discontinuities in the finished feature. Evidence role: general_support; source type: research. Supports: the technical challenges of machining continuous features on long parts. Scope note: Specific challenges vary with feature type, tolerance requirements, and part material ↩
-
"CNC Router Engineering// Fixed VS. Moving Gantry", https://www.youtube.com/watch?v=ALvNohdBHb4. In machine tool design, configurations with stationary workpieces and moving cutting heads allow continuous support along the full workpiece length without requiring support structures to move with the table, reducing dynamic loads and simplifying fixturing for long, flexible parts. Evidence role: general_support; source type: education. Supports: the support advantages of stationary-workpiece machine configurations. Scope note: This advantage must be weighed against other factors including machine rigidity, thermal stability, and axis dynamics ↩
-
"Analysis of angular-error uncertainty in planar multiple-loop structures …", https://rpk.lcsr.jhu.edu/wp-content/uploads/2016/08/Li15_Analysis-of-Angular-Error-Uncertainty.pdf. In coordinate metrology, an angular misalignment of θ radians produces a lateral displacement of approximately L×θ at distance L from the pivot point, where small angles in radians equal the angle in degrees multiplied by π/180. Evidence role: mechanism; source type: education. Supports: how angular misalignment errors propagate with distance from a reference point. Scope note: This represents the geometric relationship; actual part deviation also depends on clamping compliance and thermal effects ↩
-
"ISO 230-2:2014 – Test code for machine tools — Part 2", https://www.iso.org/standard/55295.html. ISO 230-2 defines positioning repeatability as the closeness of agreement between repeated position measurements at the same target position under the same conditions, typically expressed as twice the standard deviation of position error. Evidence role: definition; source type: institution. Supports: the standardized definition and testing methodology for machine tool axis repeatability. Scope note: Standard test conditions may not reflect all variables present during actual production machining ↩
-
"A Robust Technique to Perform Product Quality Inspection", https://scholarworks.utrgv.edu/cgi/viewcontent.cgi?article=1947&context=etd. Quality control methodology for multi-setup machining emphasizes verification of datum-referenced dimensions and feature relationships that span setup boundaries, as these are most susceptible to accumulated positioning errors, with coordinate measuring machines or laser trackers often required for long parts where conventional inspection tools cannot span the full length. Evidence role: general_support; source type: institution. Supports: inspection methodology for parts machined in multiple setups. Scope note: Specific inspection requirements depend on drawing specifications and tolerance allocation ↩
-
"How to Use the Torque Chart to Optimize Your CNC Workflow", https://tormach.com/articles/how-to-use-the-torque-chart-to-optimize-your-cnc-workflow?srsltid=AYCX9vLaW7JmgfZZU7DTtXyVDAZZhWhwr6_uFs6h2a3ZAStWqxMclvLM. CNC spindle motors typically exhibit a constant-torque region at lower speeds and a constant-power region at higher speeds, with maximum power available only above a transition speed; below this speed, available power decreases proportionally with speed while torque remains constant. Evidence role: mechanism; source type: education. Supports: the relationship between spindle speed, torque, and available power in CNC machine tools. Scope note: Specific power and torque curves vary by spindle design and motor type ↩
-
"Analysis of the Displacement of Thin-Walled Workpiece Using a …", https://pmc.ncbi.nlm.nih.gov/articles/PMC8400720/. Research on thin-wall machining demonstrates that workpiece stiffness, rather than machine rigidity, often becomes the limiting factor when wall thickness falls below approximately 3-5mm in aluminum, with deflection magnitude depending on wall geometry, support spacing, and instantaneous cutting forces. Evidence role: mechanism; source type: research. Supports: the mechanism of thin-wall workpiece deflection under cutting forces. Scope note: Specific deflection behavior varies with alloy properties, wall geometry, and cutting parameters ↩
-
"What exactly is Rigid tapping? Why people always ask does it do …", https://www.cnczone.com/forums/general-metalwork-discussion/41856-cnc.html. Rigid tapping, also called synchronous tapping, is a CNC machining method where the controller maintains precise synchronization between spindle rotation and Z-axis feed throughout the tapping cycle, eliminating the need for tension-compression tap holders by ensuring the feed rate exactly matches the thread pitch multiplied by spindle speed. Evidence role: definition; source type: education. Supports: the technical definition and operating principle of rigid tapping. ↩
-
"ISO metric screw thread", https://en.wikipedia.org/wiki/ISO_metric_screw_thread. In screw thread terminology, the lead is the axial distance a threaded part advances in one complete revolution, while pitch is the distance between corresponding points on adjacent threads; for single-start threads, lead equals pitch, but for multi-start threads, lead equals pitch multiplied by the number of starts. Evidence role: definition; source type: encyclopedia. Supports: the relationship between thread lead and pitch in single-start threads. ↩

Chris Lu
Aprovechando más de una década de experiencia práctica en la industria de la máquina herramienta, en particular con máquinas CNC, estoy aquí para ayudar. Si tiene alguna pregunta que le haya surgido a raíz de este artículo, si necesita orientación para seleccionar el equipo adecuado (CNC o convencional), si está explorando soluciones de máquinas personalizadas o si está listo para discutir una compra, no dude en CONTACTAR CONMIGO. Encontremos la máquina herramienta perfecta para sus necesidades.