

¿Cómo especificar el diámetro del mandril en función de las RPM máximas del husillo en un torno CNC?
Un folleto de torno puede indicar 5000 r/min. Un mandril grande a menudo no puede funcionar a esa velocidad. El diámetro del mandril y las RPM del husillo deben especificarse juntos, con un margen de seguridad.
El diámetro del mandril en un torno CNC se especifica en función del menor valor entre las RPM de la placa de características del husillo y la velocidad segura nominal del mandril. El límite del mandril debe estar por encima del máximo del husillo, con un margen. El tamaño se determina entonces según la pieza de trabajo, no por el cuerpo más grande del catálogo.
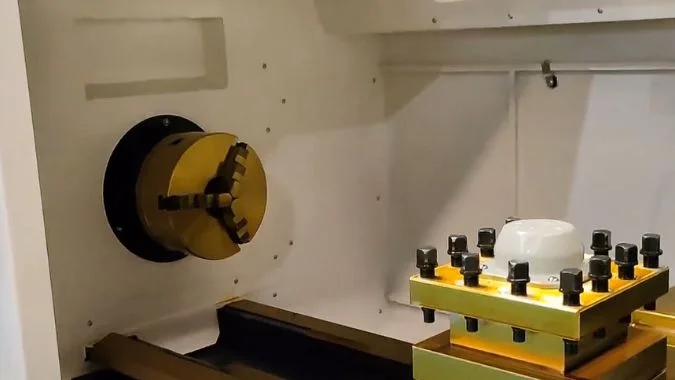
Una placa de características puede indicar 5000 r/min y aun así no ser la velocidad a la que puede ejecutarse el trabajo. El mandril tiene su propio límite. La fuerza centrífuga en las mordazas reduce la fuerza de sujeción a medida que aumentan las RPM.1. El taller utiliza entonces el menor de los dos límites. Esa diferencia se encuentra entre las RPM de la placa de características y la velocidad segura nominal del mandril.
¿Cuál es la diferencia entre las RPM de la placa de características del husillo y la velocidad segura nominal del mandril?
Los talleres utilizan las RPM máximas del husillo como límite del mandril. El mandril ya puede ser inseguro a esa velocidad. Deben compararse ambas placas de características.
Las RPM de la placa de características del husillo indican qué tan rápido puede girar el husillo o el motor. La velocidad segura nominal del mandril indica qué tan rápido puede girar el mandril manteniendo un agarre seguro. Los dos límites no son iguales. El menor es el límite operativo del taller.
Qué indica la placa de características del husillo
Las RPM de la placa de características del husillo son la velocidad permitida por el diseño del husillo. Los rodamientos, la lubricación, la potencia del motor y la estructura de la máquina determinan este valor.2. La placa generalmente muestra una velocidad nominal y una velocidad máxima. La velocidad nominal es el punto de trabajo estable. La velocidad máxima es el límite de diseño. Superarla daña el husillo. Ese número está relacionado con el motor y los rodamientos, no con la sujeción.
Qué indica la velocidad segura nominal del mandril
El fabricante del mandril establece una velocidad máxima permitida basada en la estructura, la fuerza de sujeción y la fuerza centrífuga. Más allá de esa velocidad, las mordazas se desplazan hacia afuera y el agarre disminuye. La pieza de trabajo puede desprenderse del mandril. El diámetro, el peso de la mordaza, la fuerza de sujeción y el equilibrio determinan este límite. Una familia Kitagawa lista 7000, 6000, 4500 y 3600 r/min según los tamaños.3. La curva de velocidad frente a fuerza de sujeción del proveedor es el método de verificación. El límite del mandril debe estar por encima del máximo del husillo, con un margen.
Por qué los dos límites no son intercambiables
El husillo puede girar más rápido de lo que el mandril puede soportar una pieza. El mandril también puede estar clasificado por encima de un husillo modesto. El uso diario sigue siempre el límite inferior. Mezclar ambas etiquetas en un presupuesto oculta el límite real. Un taller que solo persigue el número del husillo terminará encontrando el plato del mandril en el suelo.
| Límite | Qué mide | Qué lo determina | Qué sucede al excederlo |
|---|---|---|---|
| RPM nominales del husillo | Qué tan rápido puede girar el husillo | Rodamientos, lubricación, motor, estructura | Daño al husillo |
| Velocidad segura nominal del mandril | Qué tan rápido puede girar el mandril con un agarre seguro | Diámetro, mordazas, fuerza, equilibrio | Pérdida de agarre, la pieza puede salir despedida |
| Límite del taller | El menor de los dos | Ambas placas, más un margen | El trabajo no debe exceder esto |
¿Por qué un mandril más grande reduce las RPM utilizables incluso si el husillo puede girar más rápido?
Un cuerpo más grande parece ofrecer más agarre. A gran velocidad, proyecta más masa hacia afuera, por lo que las RPM utilizables disminuyen incluso cuando el husillo puede alcanzar mayores velocidades.
Un mandril más grande reduce las RPM utilizables porque la velocidad periférica y la fuerza centrífuga de las mordazas aumentan con el diámetro. La fuerza de sujeción disminuye, la vibración aumenta y el límite de seguridad se sitúa por debajo de la capacidad de exceso de velocidad del husillo. Más grande no es necesariamente mejor.
Velocidad lineal y el alcance
A las mismas RPM, un mandril más grande tiene una mayor velocidad periférica.4. El cuerpo del mandril y las mordazas experimentan entonces un aumento brusco de la fuerza centrífuga. El agarre puede aflojarse. La pieza puede salir despedida de las mordazas. Las RPM aumentan, las mordazas son lanzadas hacia afuera y la fuerza de sujeción disminuye. Un mandril más grande y unas mordazas más pesadas empeoran ese efecto. La pieza puede desplazarse durante el corte. Por lo tanto, el corte pesado requiere un agarre remanente a la velocidad máxima, no solo la fuerza estática del catálogo.
Rigidez y equilibrio
Un mandril grande representa una masa importante. El husillo y la brida deben sostenerlo. Un soporte débil a alta velocidad provoca vibraciones y marca la superficie. El equilibrio dinámico también es más difícil de lograr en un cuerpo grande.5. El desequilibrio a alta velocidad aumenta el ruido y la vibración.6. Las RPM utilizables disminuyen entonces para mantener el conjunto silencioso. El motor del husillo aún puede tener velocidad sin utilizar.
Adapte el cuerpo a la pieza
El diámetro nominal del mandril se ajusta al rango de la pieza y a la nariz del husillo. Ser más grande no es la opción predeterminada. La sujeción externa máxima debe superar el diámetro exterior de la pieza con un margen. Las mordazas en el último diente pierden fuerza. La sujeción interna requiere una carrera de mordaza suficiente. La brida debe coincidir con la nariz del husillo, de lo contrario el mandril no podrá montarse. Los tornos CNC horizontales suelen utilizar cuerpos de 100 a 500 mm. Los tamaños comunes incluyen 160, 260, 400 y 500 mm.7. Vertical lathes can exceed 500 mm8. Large disks want low speed and high torque. Small shafts want a stable high-speed band.
| Driver | What a larger chuck does | Effect on usable RPM |
|---|---|---|
| Rim speed | Higher at the same r/min | Safe cap falls |
| Jaw throw | More mass thrown outward | Grip decays sooner |
| Mass on the nose | More demand on spindle and flange | Vibration at speed |
| Balance | Harder to keep even | Noise and shake rise |
| Fit to the part | Only needed when the OD requires it | Extra diameter is unused risk |
¿Cómo deben calcularse la masa de las mordazas y los contrapesos dentro de la clasificación de velocidad del mandril?
A speed chart that ignores jaw mass is a paper limit. Heavy jaws and a wide grip then eat the force the nameplate still claims.
Jaw mass inside the chuck speed rating includes the base jaw, top jaw, and moving hardware. Heavier jaws and a larger center-of-gravity radius raise centrifugal force with the square of RPM. Counterweights can offset that throw.
Count the moving mass
The core check is how jaw centrifugal force offsets clamping force. Force rises with the square of speed9. Effective grip then falls. A workpiece can fly, or a jaw can fail. Heavier jaws raise centrifugal force at the same RPM, so grip loss is worse. The counted mass is one jaw: base jaw, top jaw, and connecting parts. A booster screw structure must count the whole moving mass.
Counterweights and center of gravity
Some chucks add centrifugal compensation. A reverse mechanism fights the outward throw and holds grip at higher speed. That option is part of the speed rating, not a shop add-on after the quote. Jaw center-of-gravity radius also matters. A jaw sitting farther out raises centrifugal force. Large-diameter work moves that radius out, so rated speed should fall. A wide grip on a large disk is then a lower RPM job, even on the same chuck body.
How makers set the number
Chuck makers often set maximum speed at the point where centrifugal force reaches two-thirds of maximum clamping force10. Weak points still need a strength check at that speed. Jaw-seat keys, bolts, and screws take shear and torsion. Thin keys, few bolts, or a low bolt grade fail first. Workpiece weight, center of gravity, a tailstock or steady rest, and cutting force then change the real safe speed. A safety factor belongs on the shop number. The chuck’s own plate is not the last word.
| Item to count | Why it changes the rating |
|---|---|
| Base jaw + top jaw + hardware | Moving mass sets centrifugal force |
| Booster-screw moving parts | Extra mass still throws outward |
| Center-of-gravity radius | A wider grip raises force at the same RPM |
| Counterweight / compensation | Offsets throw and can hold grip at higher speed |
| 2/3 clamping-force rule | Common maker definition of max speed |
| Keys, bolts, screws | Strength floor at that speed |
| Part weight, rest, cut force | Shop safety factor on top of the plate |
¿Por qué un folleto de “husillo de 5000 r/min” puede estar limitado a una velocidad de mandril mucho menor?
A brochure 5000 r/min is the spindle’s own ceiling. The chuck plate on the body is often far lower, and that plate is the one that binds.
A brochure 5000 r/min spindle is still capped at a lower chuck speed because the chuck and fixture set a new limit. The chuck nameplate, jaw type, balance, G50, and available torque all sit below that printed 5000.
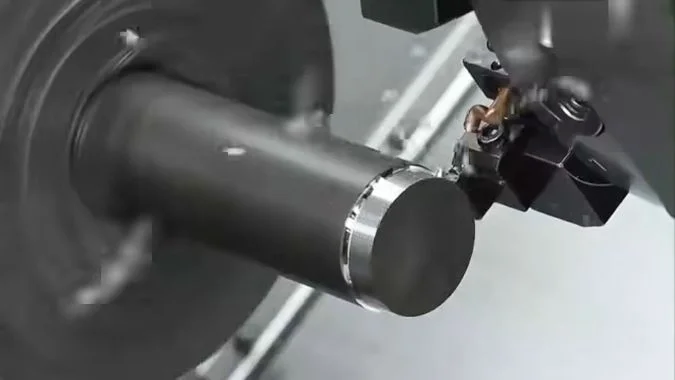
The brochure number is the spindle
5000 r/min on a CNC lathe brochure is the spindle’s own limit. In use, the chuck and fixture become the new cap. The two labels are not the same. A 5000 r/min line does not mean a chucked part may run at 5000. The chuck body and the front guard door carry the permissible speed and the permissible clamp pressure. Those are the maker’s safety bounds from strength, jaw type, and balance. The spindle must not pass them.
What else pulls the cap down
Special jaws and non-standard soft steel jaws clamp less efficiently and throw worse, so the allowed speed falls again. A nut that sits outside the chuck rim is a further cut. An unbalanced workpiece at high speed shakes the machine and the grip. Work near the chuck limit needs a balanced part and clamp pressure at the allowed maximum.
G96 constant surface speed11 is a hard program limit. As diameter falls, theoretical RPM soars. G50 must set a spindle max so the machine and the fixture stay inside strength12. G50 S2000 is one such cap. Speed then shall not exceed 2000 r/min.
High RPM also does not mean the cut can be driven. Short torque or power in the used band leaves the spindle spinning without feeding the tool. Faster spindle speed is not always better on that cut. Speed should then fall on purpose. Drive type, bearings, and lubrication already set the spindle max. Brochure values are often an ideal test. Load on the floor takes a discount.
Read the plates before the brochure
The chuck plate and the guard door are the first check. Workpiece weight, balance, and the cutting method then set a safe speed. The brochure figure is not the operating basis.
| Limit | Typical source | What it does to 5000 r/min |
|---|---|---|
| Spindle brochure | Ideal spindle test | Prints 5000 |
| Chuck nameplate | Body and guard door | New, often lower, cap |
| Special / soft jaws | Extra throw, weaker clamp | Cap falls again |
| Unbalanced part | Vibration at speed | Cap must fall |
| G96 without G50 | RPM soars as diameter falls | Program must lock a max |
| Short torque in the band | Motor cannot drive the cut | Speed should fall on purpose |
Conclusión
Specify chuck diameter only after the chuck speed limit clears the spindle max with a margin. Size then follows the part. The brochure RPM is not the shop cap.
-
"Factors affecting grip force: Anatomy, mechanics, and referent …", https://pmc.ncbi.nlm.nih.gov/articles/PMC4013148/. Engineering mechanics demonstrates that centrifugal force acting on rotating chuck jaws increases with the square of rotational velocity, creating an outward force that opposes the mechanical clamping force and reduces net gripping capacity. Evidence role: mechanism; source type: research. Supports: the inverse relationship between rotational speed and effective clamping force due to centrifugal effects. ↩
-
"Machine Tool Spindle Bearings Types & Selection Guide", https://pibsales.com/tutorials/machine-tool-spindle-bearings-types-selection-guide/?srsltid=AU7gw4Woq0f0qZH3Pq9Ku02G0SH7bVD6ib4qKPdLvf7ktGDbQzJ2yuaX. Machine tool design literature identifies bearing DN values (bearing bore diameter × RPM), lubrication system capacity, motor power curves, and structural dynamics as the principal factors establishing spindle speed envelopes, with each subsystem imposing distinct operational limits. Evidence role: general_support; source type: education. Supports: the primary engineering constraints that determine maximum spindle operating speeds. ↩
-
"Forming Quality Research on the Variable-Diameter Section …", https://pmc.ncbi.nlm.nih.gov/articles/PMC9414841/. Manufacturer specifications across the chuck industry demonstrate that maximum rated speeds decrease with increasing chuck diameter, reflecting the physics of centrifugal forces and the engineering constraints of maintaining safe clamping at higher peripheral velocities. Evidence role: case_reference; source type: other. Supports: the inverse relationship between chuck diameter and rated maximum speed. Scope note: The specific Kitagawa values cited are manufacturer-specific, though the inverse relationship is industry-wide ↩
-
"Tangential speed", https://en.wikipedia.org/wiki/Tangential_speed. Rotational kinematics establishes that tangential (rim) velocity equals the product of angular velocity and radius (v = ωr), meaning that at constant RPM, peripheral speed increases proportionally with diameter. Evidence role: mechanism; source type: encyclopedia. Supports: the linear relationship between rotational radius and tangential velocity at constant angular velocity. ↩
-
"Rotating Machinery Rotor Balancing", https://rotorlab.tamu.edu/me459/Rotor%20Balancing/Rotating_Machinery_Rotor_Balancing.pdf. Rotating machinery engineering demonstrates that balancing precision requirements become more stringent with increasing diameter and mass, as unbalance forces scale with both mass and the square of the radius, making larger components more sensitive to mass distribution asymmetries. Evidence role: general_support; source type: research. Supports: the increased difficulty of achieving dynamic balance in larger rotating components. ↩
-
"Study on the Influence of Unbalanced Phase Difference …", https://www.mdpi.com/1424-8220/25/6/1691. Vibration engineering establishes that unbalanced rotating masses generate periodic forces proportional to the square of rotational speed, producing vibration amplitudes and noise levels that increase dramatically with RPM, potentially causing surface finish degradation and accelerated bearing wear. Evidence role: mechanism; source type: research. Supports: the relationship between rotational imbalance and vibration severity. ↩
-
"Lathe Chucks: Clamp, Center, and Control Your Work", https://www.mscdirect.com/resources/buying-guides/lathe-chucks. Machine tool industry specifications document that horizontal CNC lathes commonly employ chucks ranging from small precision sizes around 100-200mm for bar work to larger capacities of 400-500mm for heavier components, with size selection driven by workpiece dimensions and machine capacity. Evidence role: general_support; source type: institution. Supports: typical chuck size ranges used in horizontal CNC lathe applications. ↩
-
"Lathe Chuck Types, Mounting & 3-Jaw vs 4-Jaw Guide", https://cncwmt.com/qa/everything-you-need-to-know-about-lathe-chuck/. Machine tool industry data indicates that vertical lathes and vertical turning centers commonly accommodate workholding fixtures ranging from 500mm to several meters in diameter, designed for large-diameter, relatively short workpieces such as rings, flanges, and disks. Evidence role: general_support; source type: institution. Supports: the typical chuck size ranges for vertical lathe configurations. ↩
-
"Centrifugal force", https://en.wikipedia.org/wiki/Centrifugal_force. Classical mechanics establishes that centrifugal force is proportional to the square of angular velocity (F = mω²r), meaning that doubling rotational speed quadruples the outward force on rotating components. Evidence role: mechanism; source type: encyclopedia. Supports: the mathematical relationship between rotational speed and centrifugal force. ↩
-
"Safe speeds for large chucks", https://www.practicalmachinist.com/forum/threads/safe-speeds-for-large-chucks.199517/. Manufacturing standards organizations document that chuck speed ratings typically incorporate safety factors where centrifugal forces are limited relative to static clamping capacity, though specific ratios vary by manufacturer and application. Evidence role: expert_consensus; source type: institution. Supports: the industry practice of setting chuck speed ratings based on centrifugal force thresholds. Scope note: The exact two-thirds ratio may be manufacturer-specific rather than a universal standard ↩
-
"G96 G-Code: Constant Surface Speed CNC Programming", https://www.cnccookbook.com/g96-g-code-constant-surface-speed-cnc/. CNC programming standards define G96 as the command that activates constant surface speed mode, automatically adjusting spindle RPM as tool position changes to maintain consistent cutting velocity at the workpiece surface. Evidence role: definition; source type: institution. Supports: the function of G96 in CNC programming standards. ↩
-
"Any tips on calculating G50 and G96 in CNC machining?", https://www.facebook.com/groups/769782850345135/posts/1298664774123604/. CNC programming standards specify that G50 with an S parameter establishes an upper spindle speed limit, preventing the spindle from exceeding a specified RPM regardless of other programmed commands, particularly important when using constant surface speed mode. Evidence role: definition; source type: institution. Supports: the function of G50 in limiting maximum spindle speed. ↩

Chris Lu
Aprovechando más de una década de experiencia práctica en la industria de la máquina herramienta, en particular con máquinas CNC, estoy aquí para ayudar. Si tiene alguna pregunta que le haya surgido a raíz de este artículo, si necesita orientación para seleccionar el equipo adecuado (CNC o convencional), si está explorando soluciones de máquinas personalizadas o si está listo para discutir una compra, no dude en CONTACTAR CONMIGO. Encontremos la máquina herramienta perfecta para sus necesidades.